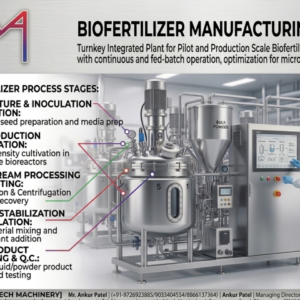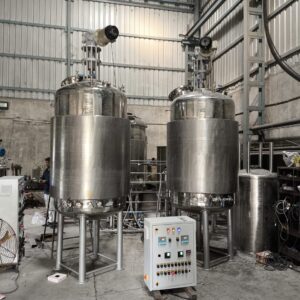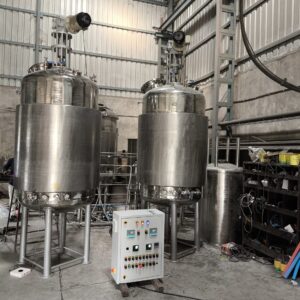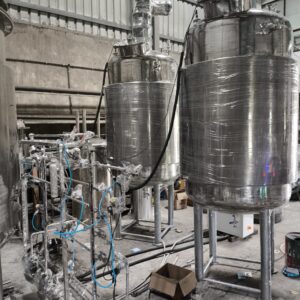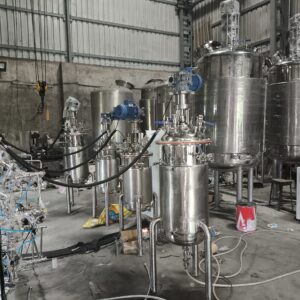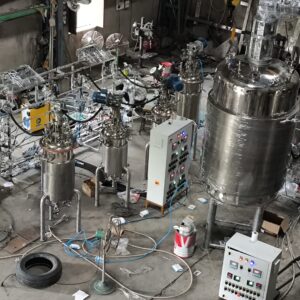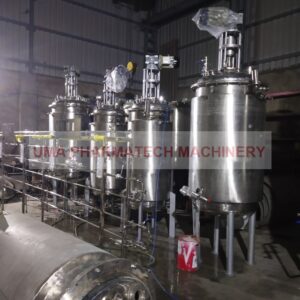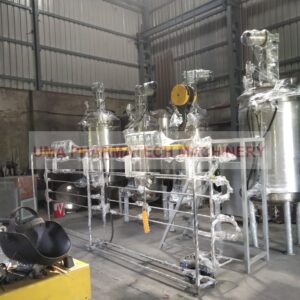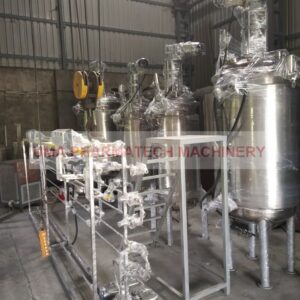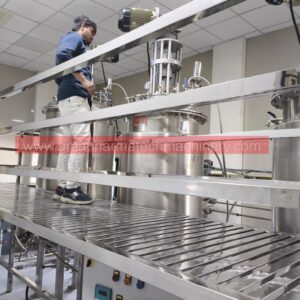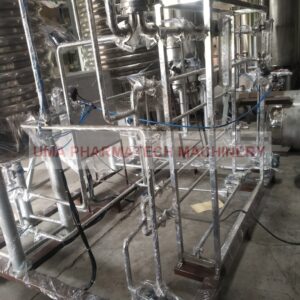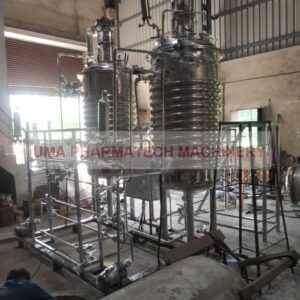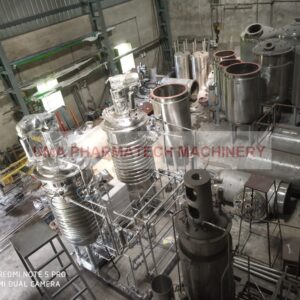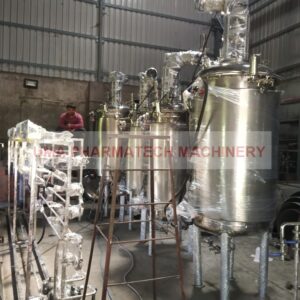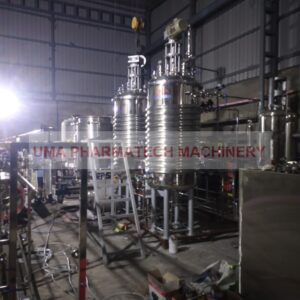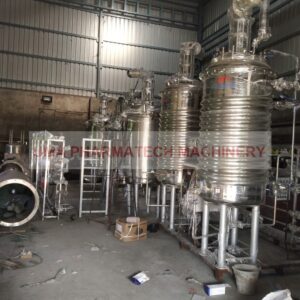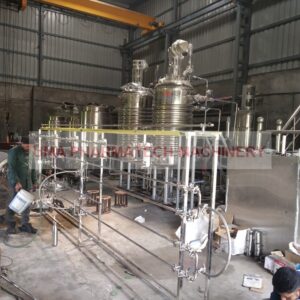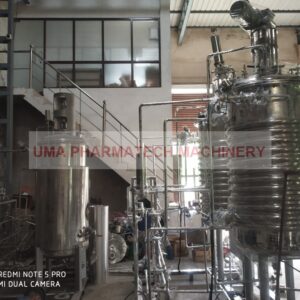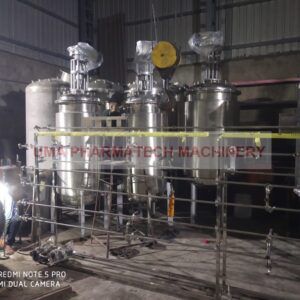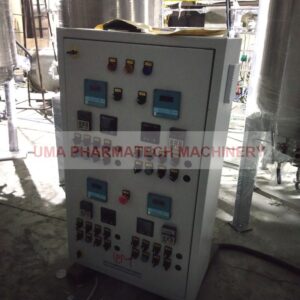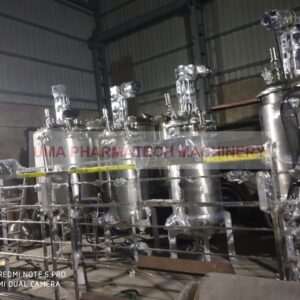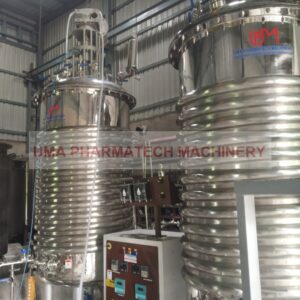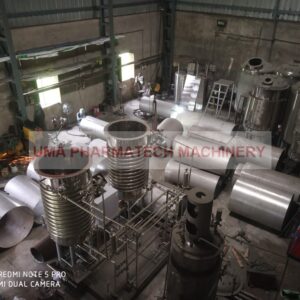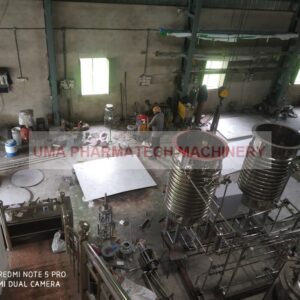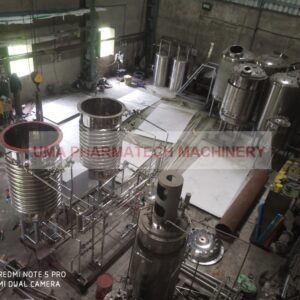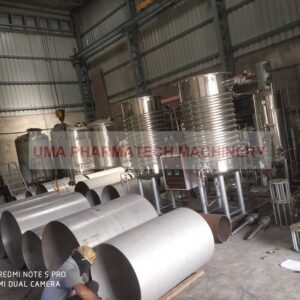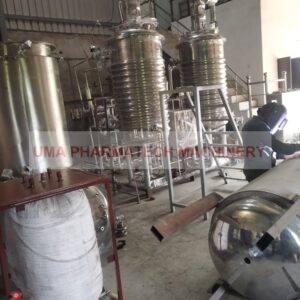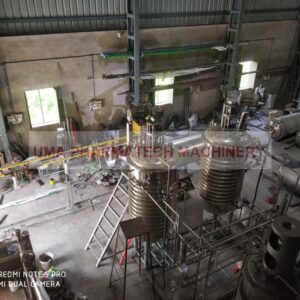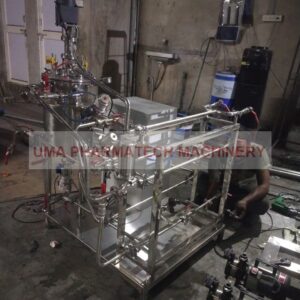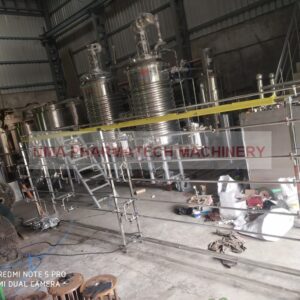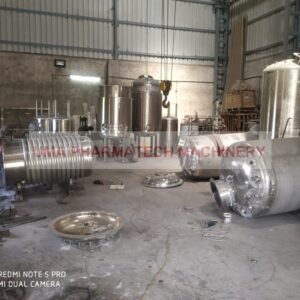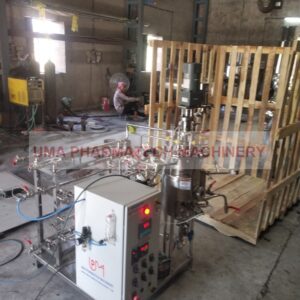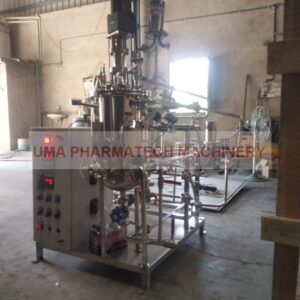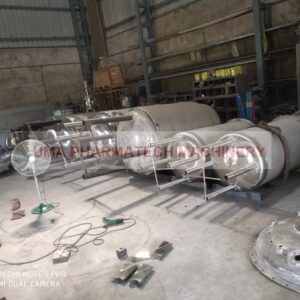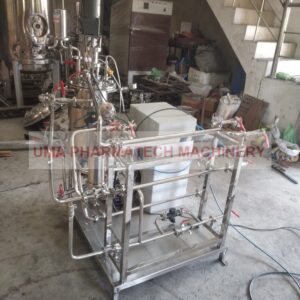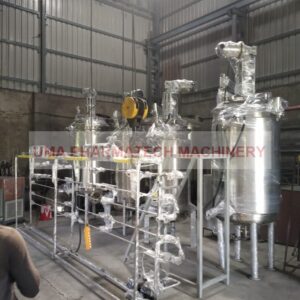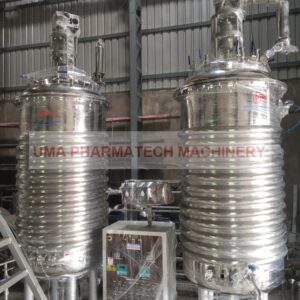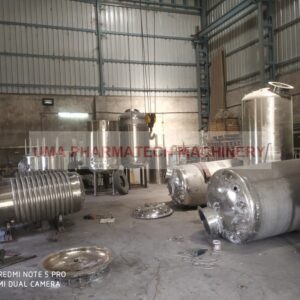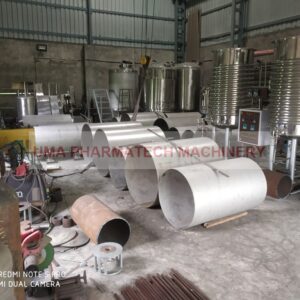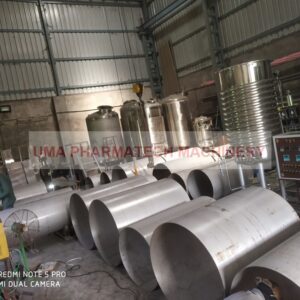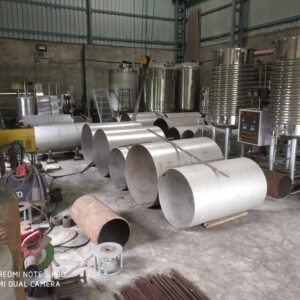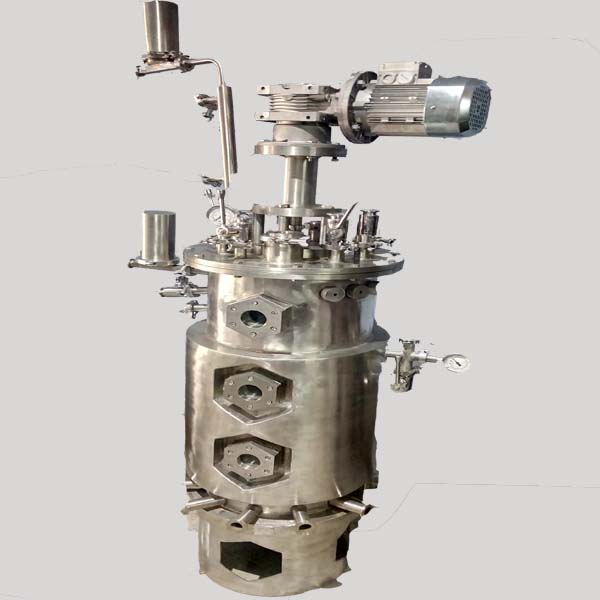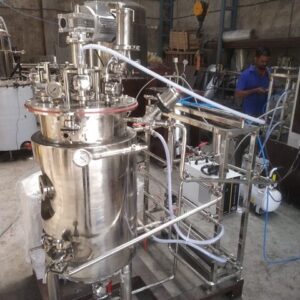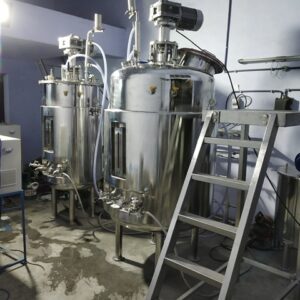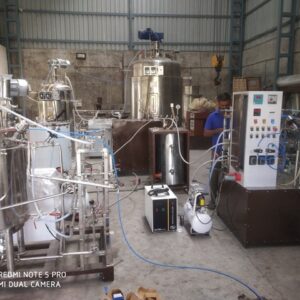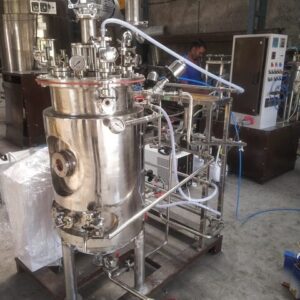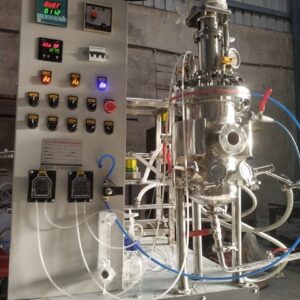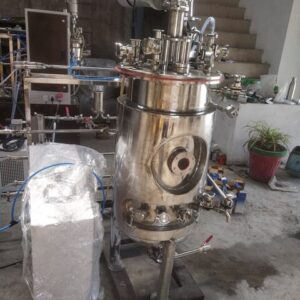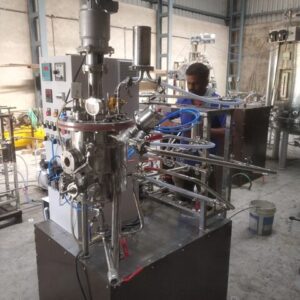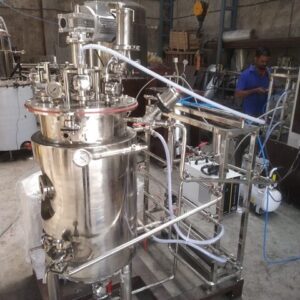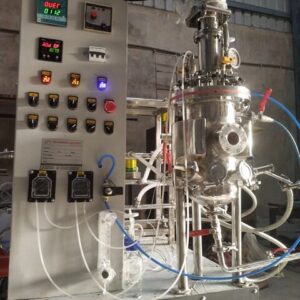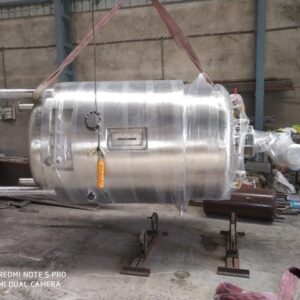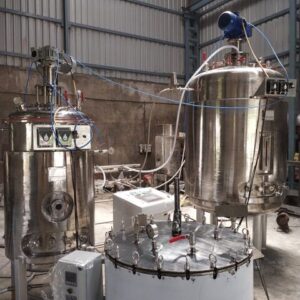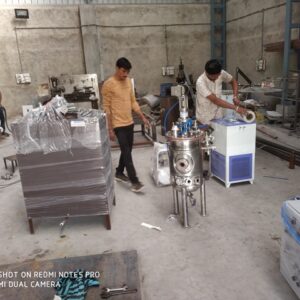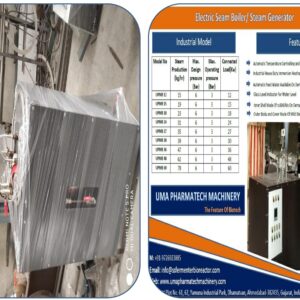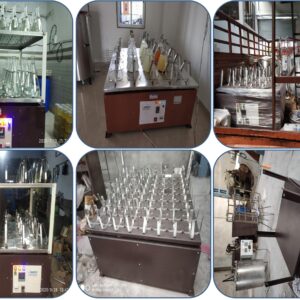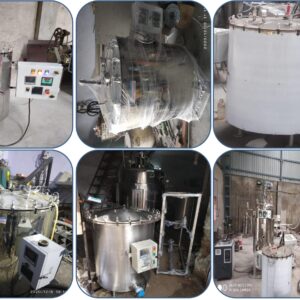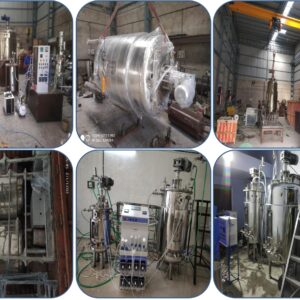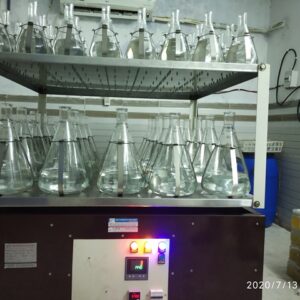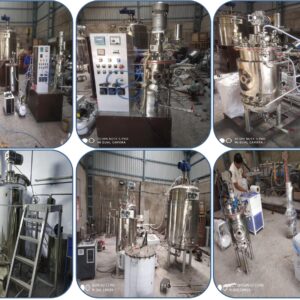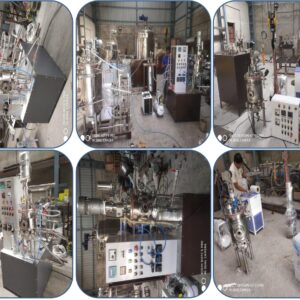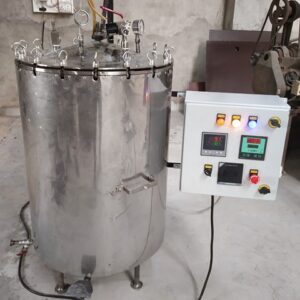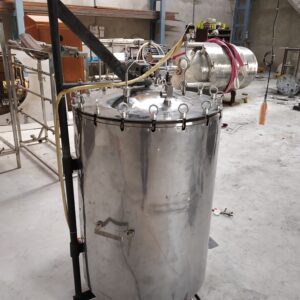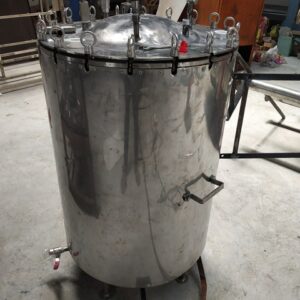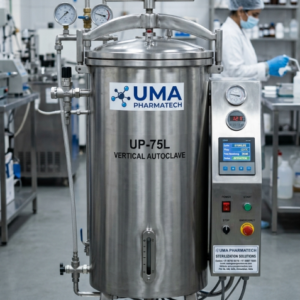
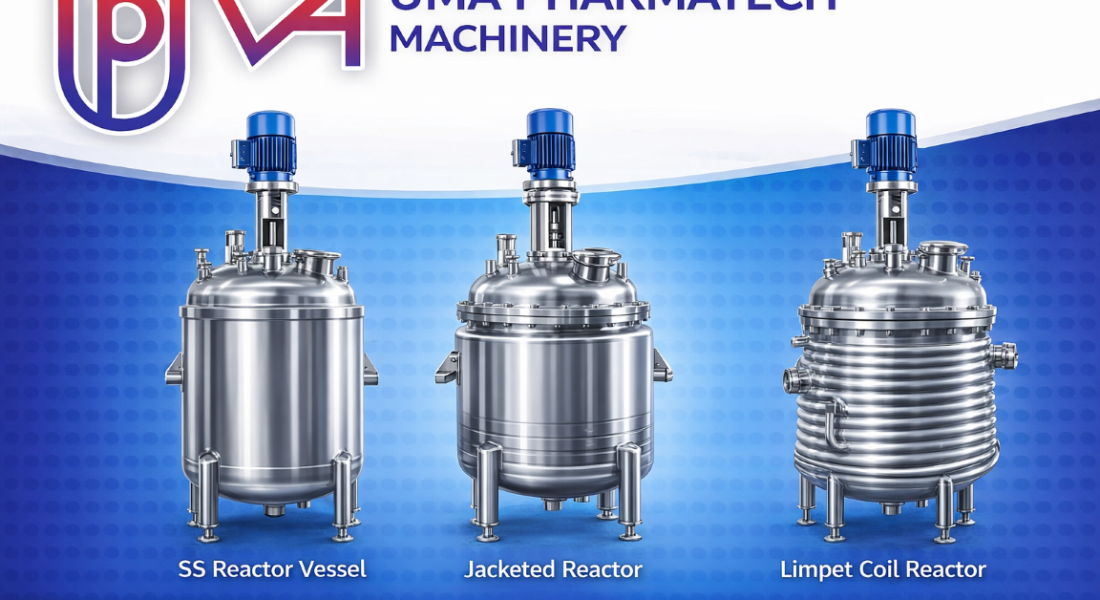
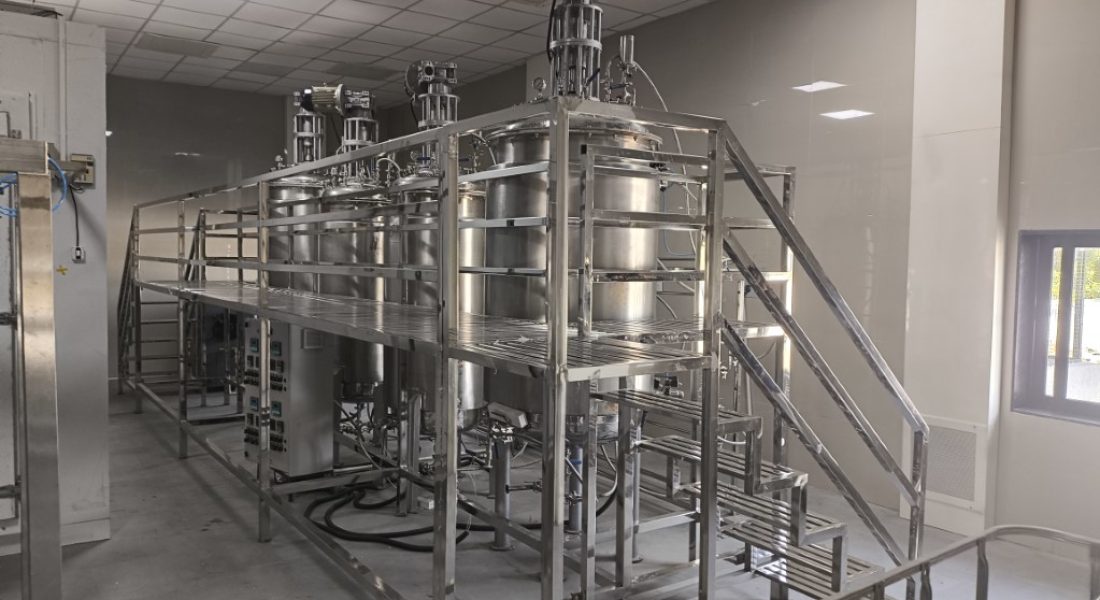
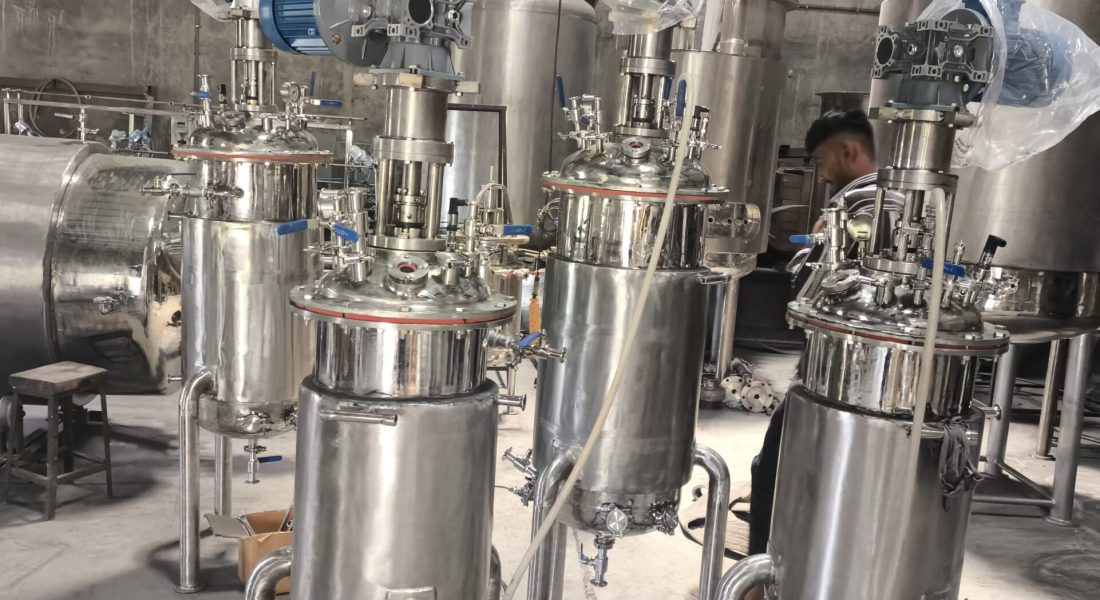
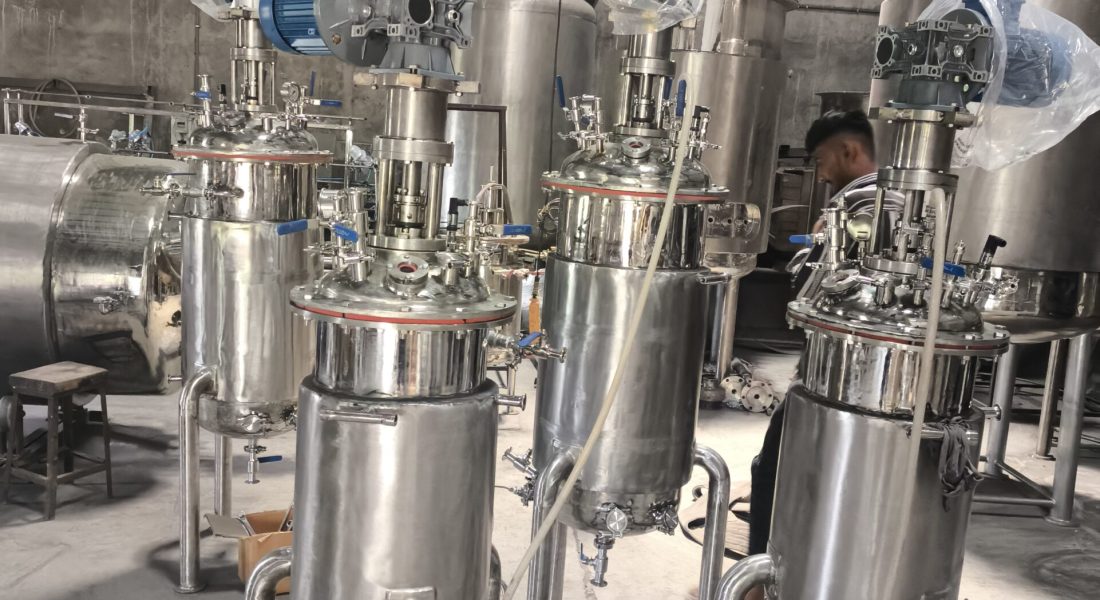
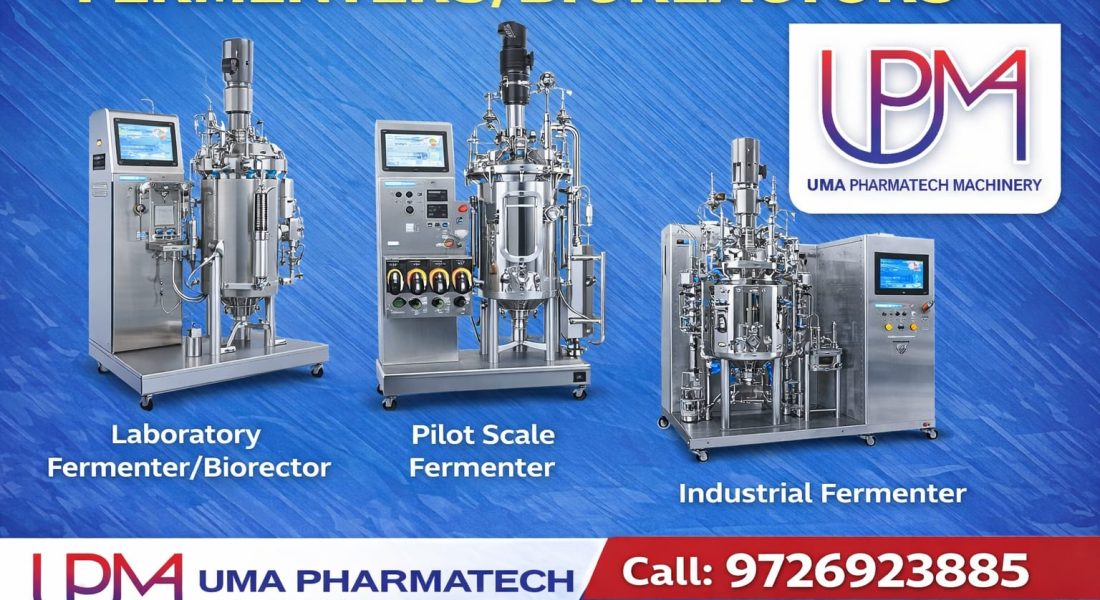
reactor for pharmaceutical industry
Showing all 4 results
-
Sale!
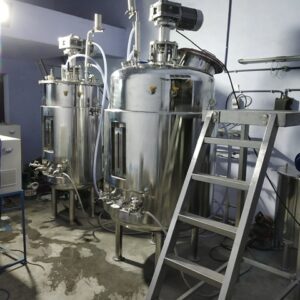
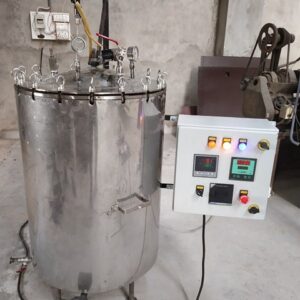
 blending tank
SS Reactor Vessel & SS Mixing Tank
Original price was: ₹650,000.00.₹625,000.00Current price is: ₹625,000.00. Add to cart -
Sale!chemical processing reactor
ss vessel
Original price was: ₹845,000.00.₹800,000.00Current price is: ₹800,000.00. Add to cart -
Sale!
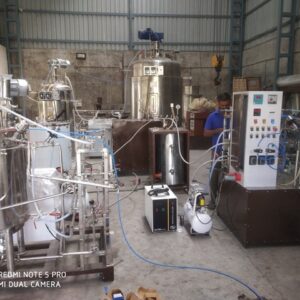
 chemical processing reactor
Stainless Steel Reactor
Original price was: ₹280,000.00.₹250,000.00Current price is: ₹250,000.00. Add to cart -
Sale!
 chemical processing reactor
Stainless Steel reactor
Original price was: ₹850,000.00.₹650,000.00Current price is: ₹650,000.00. Add to cart
High-Performance Reactor For Pharmaceutical Industry Solutions
Advanced Chemical Processing and Synthesis
Finding the right reactor for pharmaceutical industry applications requires partnering with reliable engineering experts who understand strict regulatory standards and sterile operational needs. Industrial processing demands specialized vessels capable of handling high pressures, precise thermal regulation, and corrosive chemical reactions. Major production houses located in Ahmedabad, Mumbai, Surat, and Vadodara consistently upgrade their facilities to incorporate robust mixing and synthesis infrastructure. Industrial setups based in Pune, Nashik, Nagpur, and Rajkot rely heavily on heavy-duty processing machinery to scale up active pharmaceutical ingredient manufacturing safely. When searching for a trusted manufacturer in Ahmedabad, plant operators look for custom-built fabrication options that guarantee zero contamination, smooth internal surface finishes, and long-term durability. Operating across Gujarat, Maharashtra, and Madhya Pradesh, industries benefit from localized engineering excellence that complies with global pharmacopeia guidelines.
Precision Engineering and Custom Fabrication
Modern production hubs situated in Indore, Bhopal, Jaipur, Jodhpur, and Udaipur require specialized equipment to manage complex multi-phase reactions. Sourcing units from an experienced manufacturer in Mumbai or a dependable manufacturer in Vadodara ensures seamless integration into existing plant piping and automation architectures. Facilities in southern and western sectors spanning Karnataka, Tamil Nadu, Telangana, Andhra Pradesh, and Kerala prioritize thermal efficiency and precise agitation control. Procurement specialists in Chennai, Bengaluru, Hyderabad, Coimbatore, and Madurai frequently look for trusted suppliers in Karnataka and suppliers in Tamil Nadu to minimize equipment transit times and secure rapid on-site installation support. Trusted suppliers in Gujarat and suppliers in Maharashtra play a critical role in delivering code-compliant pressure vessels that meet ASME and GMP standards.
Scalable Bioprocessing and Industrial Compliance
As chemical synthesis scales from laboratory benches to commercial manufacturing lines, operational safety remains paramount. Facilities in industrial clusters across Visakhapatnam, Thiruvananthapuram, Kochi, Kolkata, and Howrah demand versatile containment systems. Partnering with elite suppliers in West Bengal or sourcing directly from premier manufacturers in Surat ensures that every batch maintains uniform heat distribution and optimal mass transfer coefficients. Regional processing units operating throughout Punjab, Haryana, and Chandigarh also integrate advanced agitation systems to streamline complex crystallization and polymerization workflows.
To acquire precision-engineered industrial systems, reach out to Uma Pharmatech Machinery. Recognized widely among top-tier manufacturers, they deliver cutting-edge processing solutions tailored to modern production requirements.
Frequently Asked Questions (FAQs)
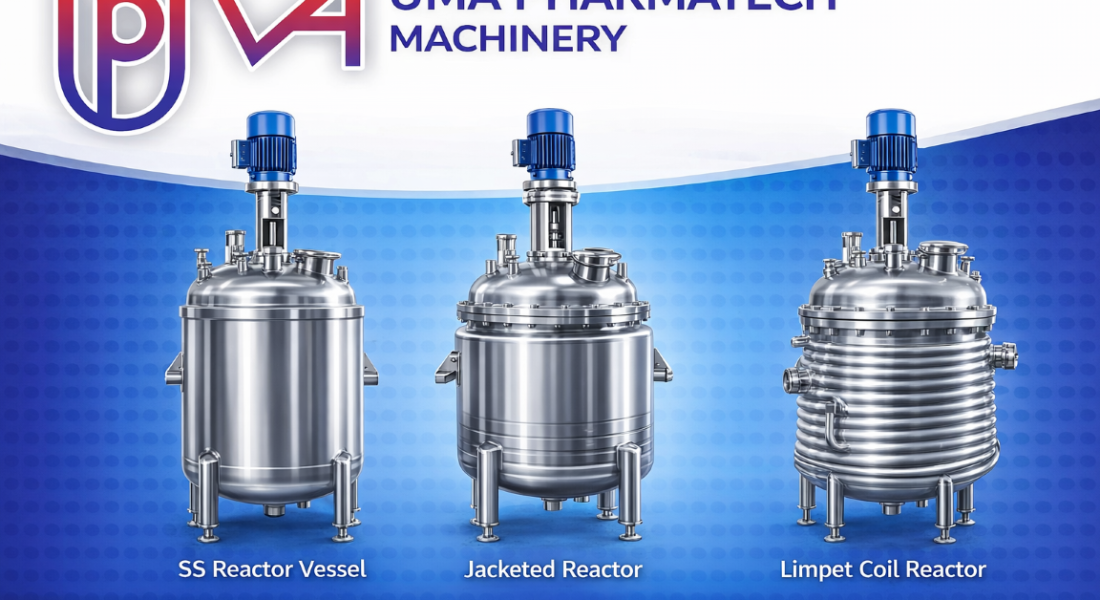
1. What types of reactors are commonly utilized as a reactor for pharmaceutical industry operations? Standard pharmaceutical processing relies heavily upon stirred-tank reactors, jacketed pressure vessels, catalytic hydrogenation reactors, and modular glass-lined or stainless steel synthesis units designed for batch and continuous manufacturing.
2. How do I select the right manufacturer for custom pharmaceutical reaction vessels? When evaluating a manufacturer in Ahmedabad or a manufacturer in Mumbai, verify their material traceability certifications, weld inspection protocols (such as radiography and dye penetrant testing), and compliance with current Good Manufacturing Practices (cGMP).
3. Why is material selection critical for a reactor for pharmaceutical industry applications? Pharmaceutical reactions frequently involve aggressive acids, organic solvents, and high-purity water systems. Utilizing high-grade austenitic or duplex stainless steel (such as SS 316L) prevents metallic leaching, corrosion, and product contamination.
4. What are the key technical specifications to review before purchasing from industrial suppliers? Buyers should closely examine design pressure limits, operating temperature ranges, agitation power ratings, seal types (such as mechanical or magnetic drives), and internal finish smoothness (Ra values below 0.5 microns).
5. How do regional suppliers ensure timely delivery and installation support for heavy reactors? Established suppliers in Gujarat and suppliers in Maharashtra coordinate closely with specialized logistics networks and technical engineering teams to provide seamless transport, site positioning, and commissioning assistance for heavy industrial machinery.